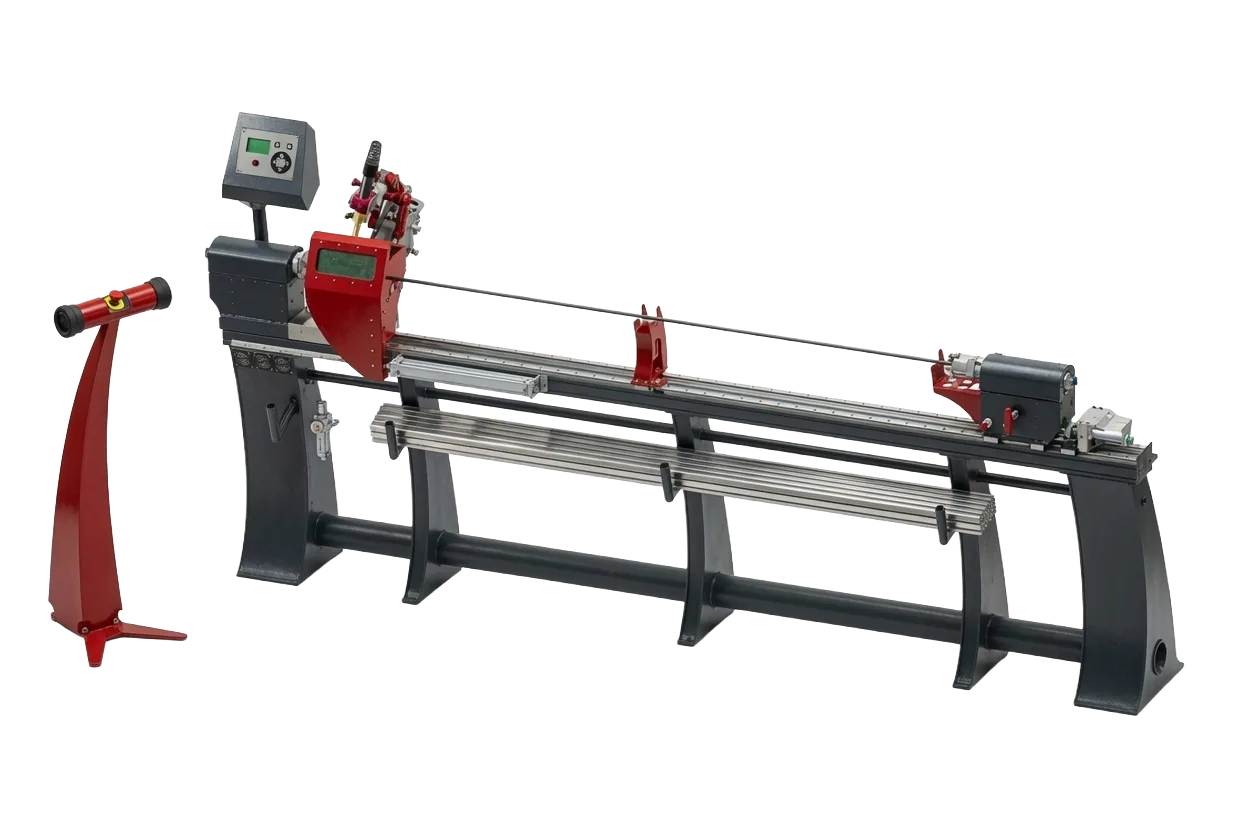
FITTER R6 is a precision automatic rotary welding machine with a maximum turning diameter of 250 mm and a maximum static load of 70 kg. The working length, defined as the distance between the spindle flanges, can be configured from 500 mm up to 7000 mm according to the customer's welding program. The spindle speed range is configured for the higher rotational speeds typically required when welding smaller-diameter, lighter workpieces.
The machine has a simple, robust mechanical construction designed for its intended load and application. It is a free-standing machine for floor installation, with anchoring to the floor recommended. The steel structure is arranged at an ergonomic working height and carries the main spindle with integrated drive. Longitudinal linear guideways extend along the machine base and carry the movable tailstock, welding arm carriage, and movable intermediate roller support. Their positions can be adapted to the length and configuration of the workpiece, providing stable support for long rod and tubular materials during welding.
FITTER R6 is designed primarily for precision production of lightweight components and for welding rod and tubular materials of different types and lengths. Precision construction and factory alignment with a maximum deviation of 0.2 mm measured at the spindle flange edges support welding of small, precise parts. This tolerance applies to the machine's factory alignment at this measurement point. The spindle through-holes also allow welding of tubular and rod material or weld-root protection with inert gas.
The movable welding arm carriage can be equipped with an integrated roller steady rest. The carriage provides a stable platform for positioning the welding arm, while the roller steady rest supports and clamps long cylindrical or rod workpieces during welding. A separate movable intermediate roller support can be positioned independently between the welding arm carriage and tailstock to provide additional support for long workpieces. The machine also includes an integrated storage rack for rod and tubular material along the front of the base.
The tailstock can be equipped with its own drive synchronized with the main spindle; both spindle drives are backlash-free. The stepper motor drives a precision planetary gearbox, which transmits motion through a belt and gear transmission.
The main spindle and tailstock spindle have identical standardized flanges, each with a 28 mm through-hole and suitable for mounting a 125 mm universal chuck. The machine can also be equipped with a fully automated pneumatic clamping system for unattended operation, using special pneumatic chucks with jaws on the main spindle and tailstock. The clamping elements for both spindles can be custom designed for the specific welding application.
Tailstock pressing uses linear motion through a drawbar, with precise mechanical adjustment of the pressure force using a control lever. Alternatively, the tailstock can be equipped with automated pneumatic pressing using a pneumatic cylinder with the required stroke.
The machine is equipped with an automatically positioned protective welding shield with a welding-filter viewing window. The shield moves pneumatically into the welding position automatically before welding begins, protecting the operator from direct exposure to the welding arc while allowing safe observation of the process.
A two-hand control device with an integrated emergency stop is used to initiate the working cycle, requiring the operator to keep both hands away from the hazardous working area during cycle start.
The welding arm has a simple pneumatic stroke and three adjustment joints. At the end of the arm, a backlash-free torch support provides +/- 15 mm two-axis adjustment and 90° rotation with position locking in five steps.
The HST CREATIVE CW 03 cold wire feeder can be fully controlled by the RCS 06 system, with adjustable feeding parameters and reverse wire feeding. The digital Remote Control Mighty Controller is available for increased operating flexibility.
The RCS 06 control system is developed for advanced welding automation. Its functions for circumferential welding include rotary acceleration and deceleration, welding source control with separate programming, advanced welding power regulation, integrated control of the cold wire feeder, program storage, and program sequences.